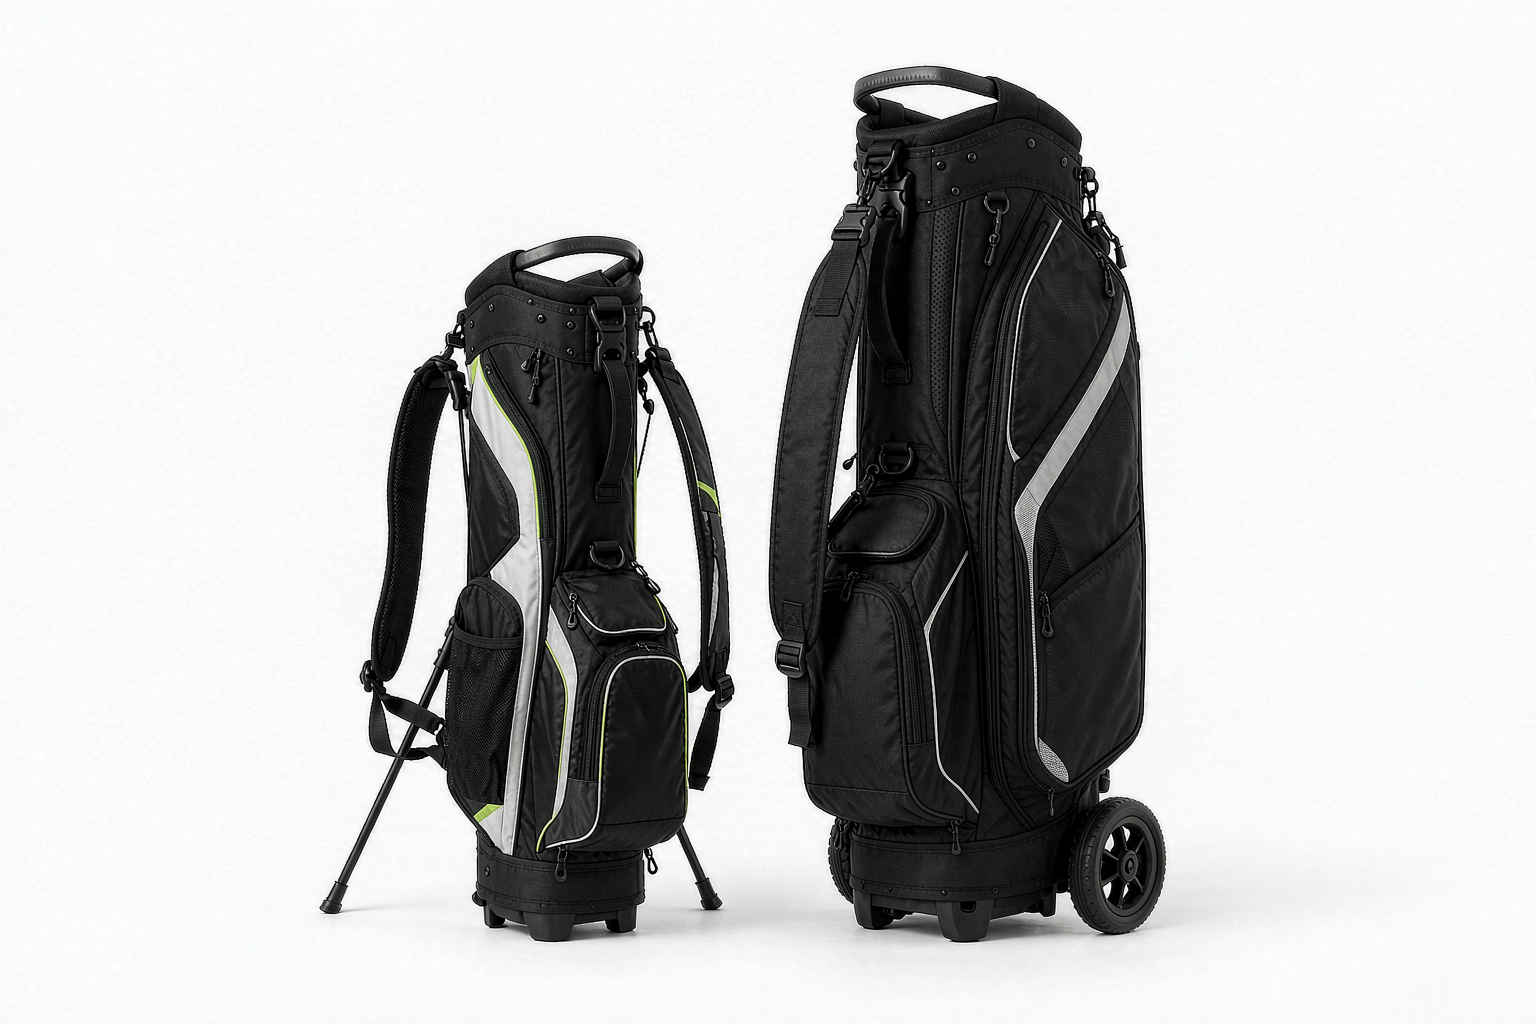
A stand bag and a cart bag look like variations of one product and behave like two different programmes. The stand bag is a weight problem with a bought-in mechanism at its centre; the cart bag is a volume problem with a structural base at its centre. Choosing between them is a question about the course, the channel, and the tooling budget rather than about styling, and the two do not share a bill of materials in any meaningful way.
Two Briefs, Two Bill of Materials
The clearest way to see the difference is to put the two side by side before any design work starts.
| Stand bag | Cart bag | |
|---|---|---|
| Weight target | 2.0–2.8 kg | 3.0–4.5 kg |
| Pattern pieces | 40–60 | 50–80 |
| Principal tooling | Leg mechanism, base mould, top mould | Flat base mould, top mould |
| Divider count | Commonly 4-way or 6-way | Commonly 14-way |
| Working MOQ | 500–800 | 500–1,000 |
| Dominant risk | Mechanism failure | Base and strap-channel failure |
Reading across the table, the trade is consistent. The stand bag is lighter and more complex mechanically, because the leg mechanism and its pivots are the hardest part to specify and the most likely to fail. The cart bag is heavier and simpler mechanically but more expensive in material, because it carries more fabric, more pockets, and a larger moulded top.
The Leg Mechanism: Tooling and Failure Modes
The leg mechanism is the defining component of a stand bag and, in most programmes, the largest single source of returns. It is usually bought in rather than manufactured, which means the specification has to name a performance rating rather than a supplier part.
Three failure modes account for most of the complaints.
- Cycle fatigue. The mechanism simply wears out. A rating in open-and-close cycles, verified on a jig rather than by hand, is the only defence, and a mechanism rated for a few thousand cycles will not survive a season of regular play.
- Deployment failure. The legs do not clear the base, or they need the bag set down carefully to deploy. This is a geometry question shared between the mechanism and the base mould, and it cannot be fixed by changing the mechanism alone.
- Retention failure. The legs deploy when they should not, which matters most on a trolley where a deployed leg catches the frame. Any bag sold as a hybrid needs a retention check under vibration.
A cart bag has no equivalent component, which is the main reason it is the simpler programme of the two to run.
Base and Divider Engineering Differences
The base does a different job in each construction. On a stand bag it carries the leg pivots and takes the impact of being set down, so it is shaped for deployment and reinforced at the pivot points. On a cart bag it has to sit square on a trolley bracket and accept a recessed strap channel, so it is shaped for a flat contact patch and shaped around the strap path.
Dividers diverge for the same reason weight does. A stand bag commonly runs a 4-way or 6-way top, because every divider adds mass that the player carries for four hours. A cart bag can run a 14-way top without penalty, because the trolley carries the load, and the separation is what the cart player is paying for. Since each divider count is its own mould, this is not a decision that can be revisited cheaply.
What Each Construction Costs
The two constructions spend their money in different places, which is why a unit-price comparison alone is misleading.
- Stand bag. Higher tooling, because the leg mechanism and its pivot reinforcement sit on top of the top and base moulds. Lower material cost, because there is less fabric and fewer pockets.
- Cart bag. Lower mechanical tooling, but higher material and labour cost driven by pocket count, a larger moulded top, and full-length dividers. Higher freight cost per unit, because the packed volume is larger.
For a programme deciding where to put its first tooling money, the practical read is that a stand bag needs more capital up front and a cart bag costs more per unit for longer. Which is preferable depends entirely on whether the constraint is cash or margin.
Which Construction Suits Which Channel
The course decides it first. Walking courses, and markets where carrying is normal, sell stand bags. Cart and trolley courses sell cart bags. This is not a preference to be argued with, and getting it wrong produces a range that does not sell regardless of how well it is made.
The channel decides the rest. Club shops and on-course retail tend to sell the higher-specification version of whichever construction their course dictates, and they will support a stand bag with a genuinely good mechanism at a higher price. Off-course and volume retail tends to sell cart bags, because the larger pocket count and the forward-facing feature set photograph and floor-display better.
Corporate and team programmes are the exception: they buy staff bags and cart bags for branding area rather than for play, and they are specified on embroidery space and lead time rather than on carry comfort.
Field Failure Patterns Compared
Two constructions, two distinct return profiles. Knowing which to watch for changes what the inspection plan should emphasise.
- Stand bag returns concentrate in the leg mechanism and at the strap anchors, which are the highest-load points on the bag. Bar-tack reinforcement at every anchor is cheap insurance.
- Cart bag returns concentrate in the base moulding and around the strap channel, where a channel that is too shallow lets the strap crush the pockets behind it, and a base that is too thin cracks under clamp load.
- Both suffer from zipper failures on the apparel pocket, which takes far more abuse than most briefs allow for. A heavier gauge there costs very little.
Two dimensional details prevent most of it: a base wall of at least 2.5 mm behind the strap channel, and pivot reinforcement around a 5–6 mm pin. Both cost very little at the tooling stage and are effectively impossible to add afterwards. The same logic applies to strap anchors — bar-tacking every one of them adds a small amount to unit cost and removes the return category that typically accounts for roughly 20% of warranty claims on a carried bag.
Reorder Timing by Construction
The two also run on slightly different clocks. A stand bag programme usually needs 30 to 45 days of tooling, because the pivots and the mechanism add fitting time, against 20 to 30 days for a cart bag with fewer moving parts. Both then need 40 to 60 days of bulk production after golden-sample approval.
The two also reorder differently. Stand bags are more seasonal, tracking the start of the walking season, so the reorder decision is a single concentrated bet timed to the spring. Cart bags sell more evenly across the season and into the corporate gifting period, which makes them easier to reorder against but harder to forecast in a single drop.
Where a range carries both, the useful effect is that the production calendar smooths out: stand bag tooling and bulk sit in the autumn and winter, cart bag reorders run through the spring and summer. That is a genuinely good reason to carry both once the range is established, even though carrying both at launch is usually one programme too many.
Get a Custom Bag Quote
The construction choice sets the tooling, the unit cost, and the return profile at the same time, so it is worth settling with real numbers rather than on preference. Share the target course type and channel, and the cost and risk comparison comes back for your own volumes: Request a quote →
Related: How to plan a range across the main golf bag types · What to specify for cart and trolley compatibility
Frequently Asked Questions
Which is cheaper to develop, a stand bag or a cart bag?
A stand bag needs more capital up front because of the leg mechanism and pivot reinforcement. A cart bag needs less tooling but costs more per unit for longer, driven by pocket count, a larger moulded top, and higher freight per unit.
Why do stand bag legs fail so often?
Cycle fatigue, usually because the mechanism was bought to a price rather than to a stated cycle rating. Ask for the rating and have it verified on a jig rather than by hand.
Why does a cart bag crush its own pockets?
Because the strap channel is too shallow. The channel has to be recessed so the cart strap sits below the pocket plane; padding the strap does not solve the problem.
How many dividers should each construction use?
Stand bags commonly use 4-way or 6-way tops because every divider adds carried mass. Cart bags commonly use 14-way because the trolley carries the load. Each count is a separate mould.
Which construction sells better?
It depends entirely on the course. Walking courses and markets where carrying is normal sell stand bags; cart and trolley courses sell cart bags. The channel decides the specification tier on top of that.
Should a new range launch with both?
Usually not. Carrying both from launch is typically one programme too many, and each construction needs its own sampling rounds. Once the range is established, carrying both does smooth the production calendar.
Buyers comparing suppliers can review our golf bags for OEM/ODM specs, materials, and MOQ.